 English
 Russian
Engineering Challenges in High-Speed VSI Rotor Operations
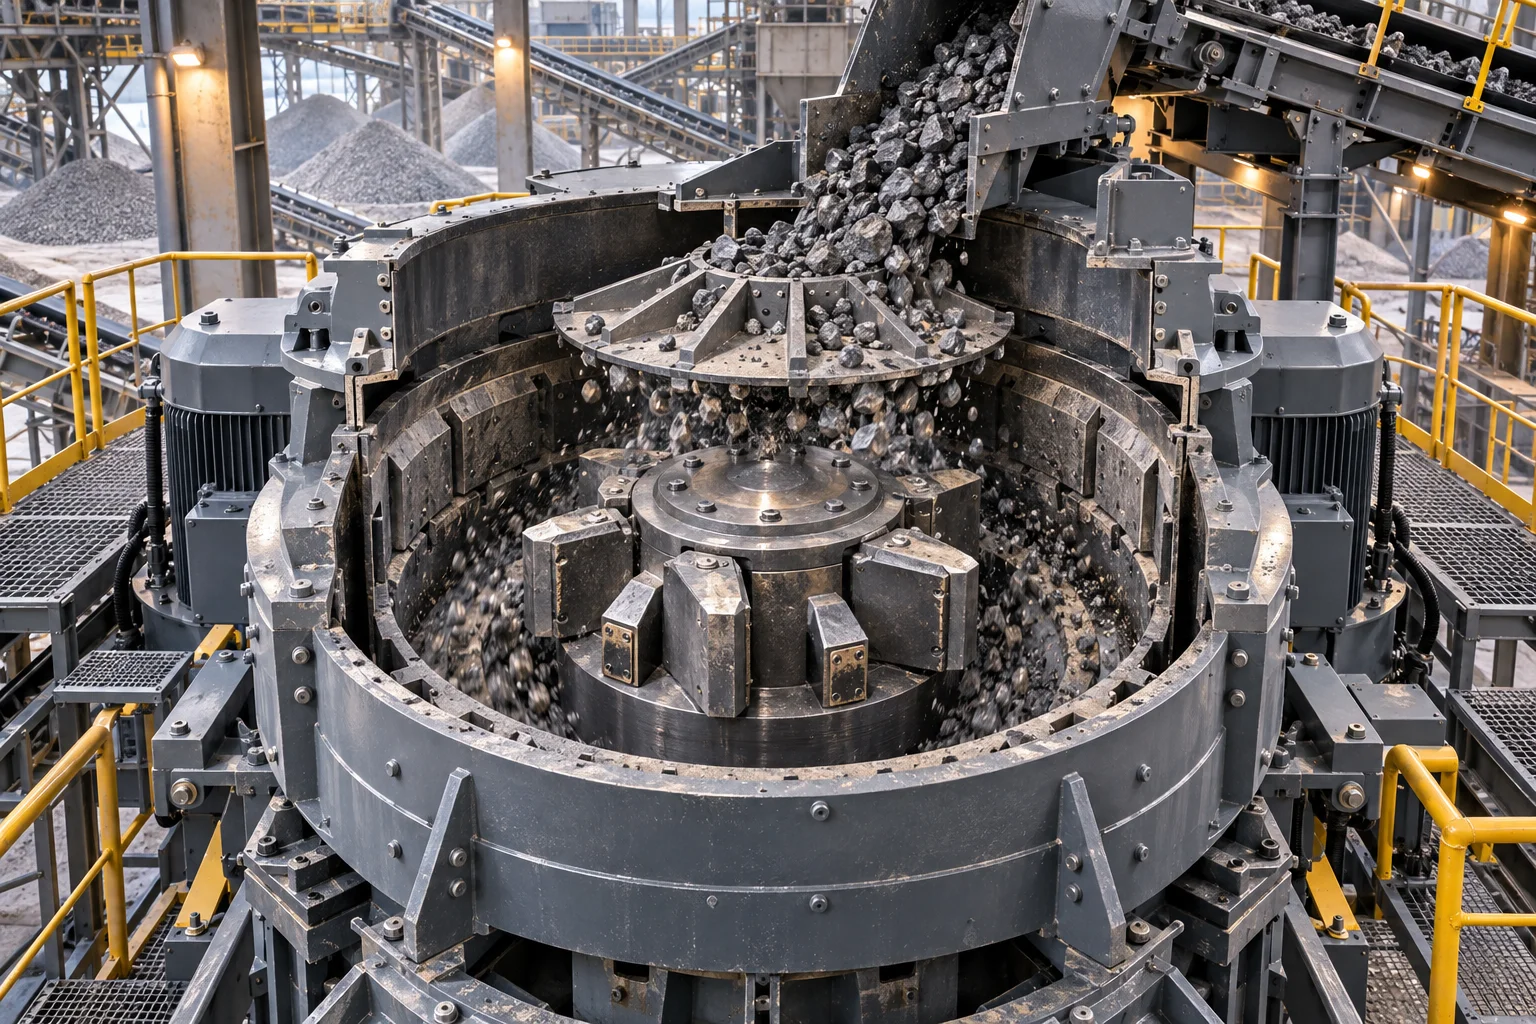
In manufactured sand production lines, Vertical Shaft Impact (VSI) crushers serve as the core shaping and tertiary crushing unit. Operating at linear speeds ranging from 60 to 85 m/s, the rotor experiences extreme abrasive wear, impact fatigue, and centrifugal stress. Rotor wear parts—including rotor tips, backup tips, distributor plates, and wear plates—represent a significant portion of aggregate operating expenditure. Achieving extended wear life requires a systematic approach combining metallurgical selection, dynamic balance maintenance, and optimized stone-on-stone autogenous chamber lining.
Metallurgical Selection: Balancing Hardness and Impact Toughness
Standard high-manganese steel is unsuitable for VSI rotor wear tips due to insufficient work-hardening under high-speed sliding abrasive contact. Sanming Machinery adopts premium tungsten carbide composite inserts vacuum-brazed onto alloy structural steel matrices. The grade selection depends on silica content and aggregate hardness:
High-Silica Quartz & Basalt (SiO2 > 65%): Coarse-grain WC-Co inserts with 8-10% cobalt binder offer superior abrasion resistance and micro-chipping resistance under severe impact.
Limestone & River Gravel: Fine-to-medium grain tungsten carbide with enhanced matrix bonding prevents premature carbide dislodgement caused by high washing velocities.
Deep-Cavity Rotor Design: Enhances internal material buffering, creating a self-protecting rock lining that absorbs 70% of kinetic energy, shielding the rotor steel body from direct erosion.
Rotor Dynamic Balancing and Vibration Control
Vibration is the primary cause of premature main bearing failure and structural cracking in VSI crushers. Rotor tips must always be replaced in diametrically opposed pairs, with individual weight deviations kept within strictly controlled tolerances:
Pair Weight Matching: Weight difference between opposing wear tips must not exceed 2 to 3 grams.
Dynamic Balance Standard: The fully assembled rotor assembly should adhere to ISO 1940 Grade G2.5 balance precision.
Vibration Sensor Integration: Continuous real-time monitoring of velocity RMS values (acceptable operating zone: < 4.5 mm/s; alert threshold: 7.1 mm/s).
Technical FAQ: VSI Rotor Operation
Q1: Why do new rotor tips wear out prematurely within 30-50 hours?
Premature wear typically stems from improper material layer formation inside the rotor pockets. If the feed contains excessive fines (< 4mm) or moisture exceeding 3%, sticky cakes cannot form the autogenous bed, exposing bare steel and carbide tips to direct scouring. Always maintain proper gradation with a maximum feed size under 45mm.
Q2: Can worn rotor tips be rebuilt via hardfacing welding?
Tungsten carbide wear tips cannot be rebuilt by hardfacing because thermal stress induces micro-cracking and detachment of the carbide inserts. However, the rotor body structural base and trail plates can be surfaced using chromium carbide hardfacing wires, provided stress-relief and preheating procedures are rigorously observed.